XEBEC Deburring Tool Path Data Format
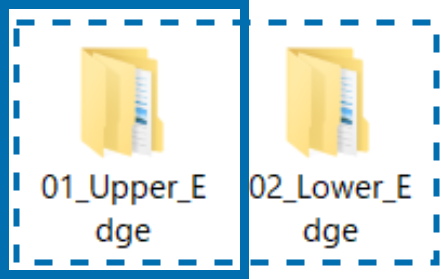
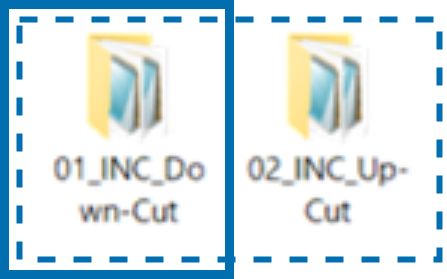
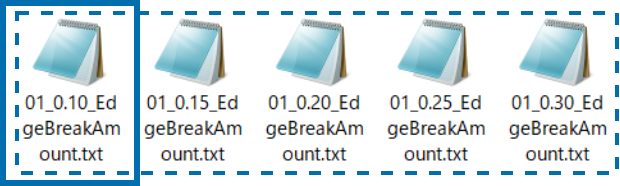
XEBEC Deburring Tool Path data is stored in separate folders as shown below.
■First Folder Level
|
|
▼ |
|
■Second Folder Level
|
|
▼ |
|
■Third Folder Level
|
|
▼ |
|
■XEBEC Deburring Tool Path Specifications are listed at the top in parentheses ( ) |
|
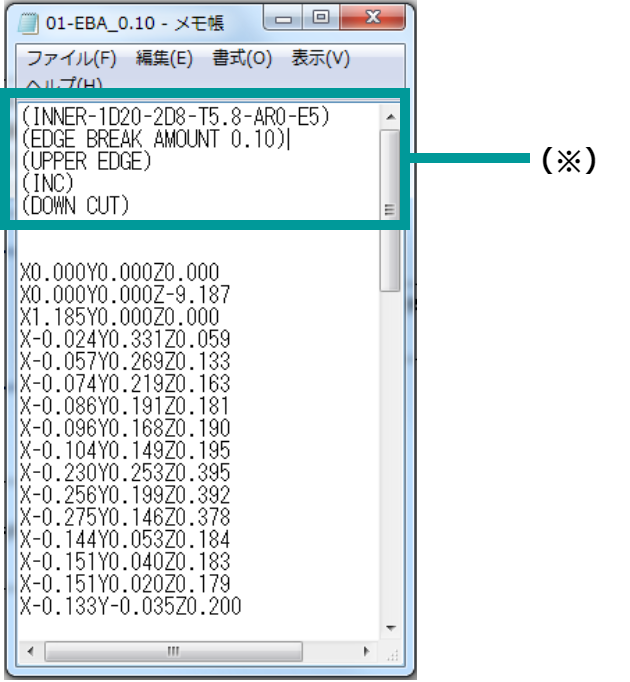
 |
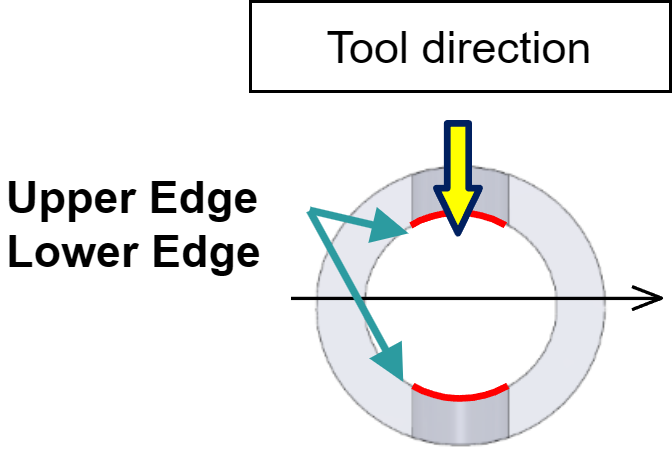
For XEBEC Deburring Tool Path for XZC-axis turn-mill machines, the data set exist only for the Upper Edge of both Outer and Inner Diameter cross holes. In that case, a total of 10 text files is provided. |
Data Example
For example, a total of 20 text files are included for an Inner Diameter cross hole.
- First Folder Level(2 Folders)
Upper Edge and Lower Edge - Second Folder Level(2 Folders)
Incremental (INC) Up Cut / Down Cut - Third Folder Level(5 Text Files)
Each text file corresponds to a specific deburring amount (edge break length)
Examples of XEBEC Deburring Tool Path Specifications
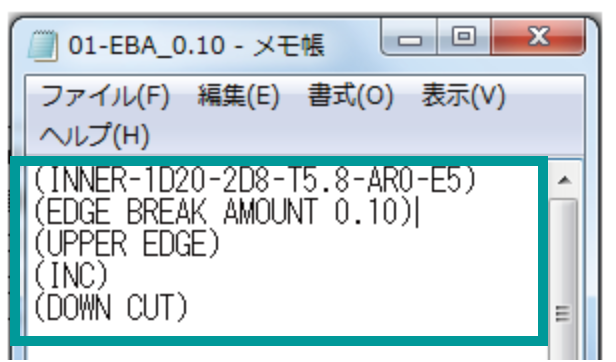
Example: On-center/Off-center Cross Hole XZY Machine Axis
(INNER-1D20-2D10-T5.8-E5);
(EDGE BREAK AMOUNT 0.10);
(DIAMETR);
(UPPER EDGE);
(INC);
(DOWN CUT);
Example: Orthogonal Cross Hole XZC Machine Axis
(INNER-1D20-2D10-T5.8-E5);
(EDGE BREAK AMOUNT 0.10);
(DIAMETR);
(UPPER EDGE);
(INC);
(DOWN CUT);
Specifications |
Descriptions |
(INNER-1D20-2D10-T5.8-E5) |
INNER: Inner Edge [OUTER: Outer Edge] |
(EDGE BREAK AMOUNT 0.10) |
Deburring Amount 0.10mm |
| (DIAMETR) | X-axis Controller Mode: Diameter [RADIUS: Radius] |
(UPPER EDGE) |
Upper Edge [LOWER: Lower Edge] |
(INC) |
Positioning Format: Incremental |
(DOWN CUT) |
Down Cut Machining [UP CUT: Up Cut Machining] |
|
Specifications in the table above are applicable to XEBEC Deburring Tool Path for XZY turn-mill machines and XZC turn-mill machines |